- This topic is empty.
-
AuthorPosts
-
22/10/2026 at 17:04 #82589
Industry Background and the Problem Facing Metallurgy and Heavy Industrial Projects
Industrial valve users across the metallurgy, oil and gas, chemical, power station, and water treatment sectors continue to confront a familiar set of technical pressures. Valve stem leakage in hazardous media, corrosion and material degradation in marine and aggressive chemical environments, seal failures under cryogenic and high-pressure conditions, erosion and wear caused by severe service applications, and increasing requirements for fugitive emission control are recurring engineering challenges. On top of these, project owners must ensure compliance with international standards such as API, CE, ISO, and ASME, while also managing valve reliability, lifecycle cost control, supply chain stability, customized engineering requirements, and consistent quality across large-scale industrial projects.
For major industrial installations in the Middle East — where metallurgy, oil and gas, and power generation projects often demand both high-pressure performance and engineering customization — these pain points become even more pronounced. This is the environment in which XINTAI Valve Group Co., Ltd., founded in 1998 and headquartered in Wenzhou, China, has built its position as an established global manufacturer specializing in industrial valves for the oil and gas, chemical, power station, water treatment, metallurgy, and mechanical markets, with business coverage extending across North America, South America, Europe, Central Asia, the Middle East, and Southeast Asia.
Authoritative Analysis: What Makes a Valve Supplier Capable of Serving Metallurgy and High-Pressure Projects
Necessity. Metallurgy and other heavy industrial projects require valves that can reliably handle elevated operating pressures while also accommodating project-specific engineering requirements. A supplier’s ability to combine standardized quality with customization directly affects long-term operational safety and cost control.
Principle Logic. XINTAI Valve Group addresses this through an integrated supply chain, with internal ownership of casting foundries and machining bases that enables full-process quality control, optimized costs, and reliable supply stability. This is paired with smart manufacturing capability — advanced automation featuring 13 six-axis robots that improve production efficiency by 40%, helping ensure consistent quality and reduced manufacturing variation. Precision engineering, supported by advanced machining and inspection systems, delivers micro-level tolerances suited to demanding flow control applications, including valve stem leakage prevention in hazardous media and seal failure risks under high-pressure conditions.
Standard Reference. The company’s certification portfolio provides the benchmark framework that metallurgy and industrial project owners typically require: ISO 9001, ISO 14001, and ISO 45001 management system certifications; CE Certification and EU Declaration of Conformity; PED; API 600, API 602, API 6D, API 607, and API 6FA; ISO10497 and ISO15848-1; API 624; SIL; EAC; PAT and TAT Certification; and Petronas and Petrobras Certified Supplier Designations.
Solution Path. On the technical side, XINTAI Valve’s operational pressure capability extends up to Class 2500, supported by a yearly manufacturing capacity of 270,000 valves. Platform compatibility spans API 6D, API 602, API 600, DIN, JIS, and GOST standards, with manual, pneumatic, and electric actuator options. The service model itself is structured around hardware supply and custom valve engineering, supported by large-scale delivery capability rooted in integrated casting and machining operations.
Deep Insights: Trends Shaping Valve Procurement for Metallurgy and Major Industrial Projects
Several trends are visible in how the industrial valve sector is evolving, based on XINTAI Valve’s own technology platform and market footprint. On the technology side, automation is becoming a differentiator rather than an option — the deployment of 13 six-axis polishing and inspection units reflects a broader shift toward robot-assisted manufacturing to achieve both efficiency gains and dimensional consistency across large production volumes.
On the market side, global business coverage spanning North America, South America, Europe, Central Asia, the Middle East, and Southeast Asia illustrates how valve demand is increasingly distributed across regions with distinct project standards and operating conditions. Export data shows 20% of products distributed to Europe and the USA, with 80% distributed to other global regions — an indication that demand for compliant, certified valve solutions is broad-based rather than concentrated in a single market.
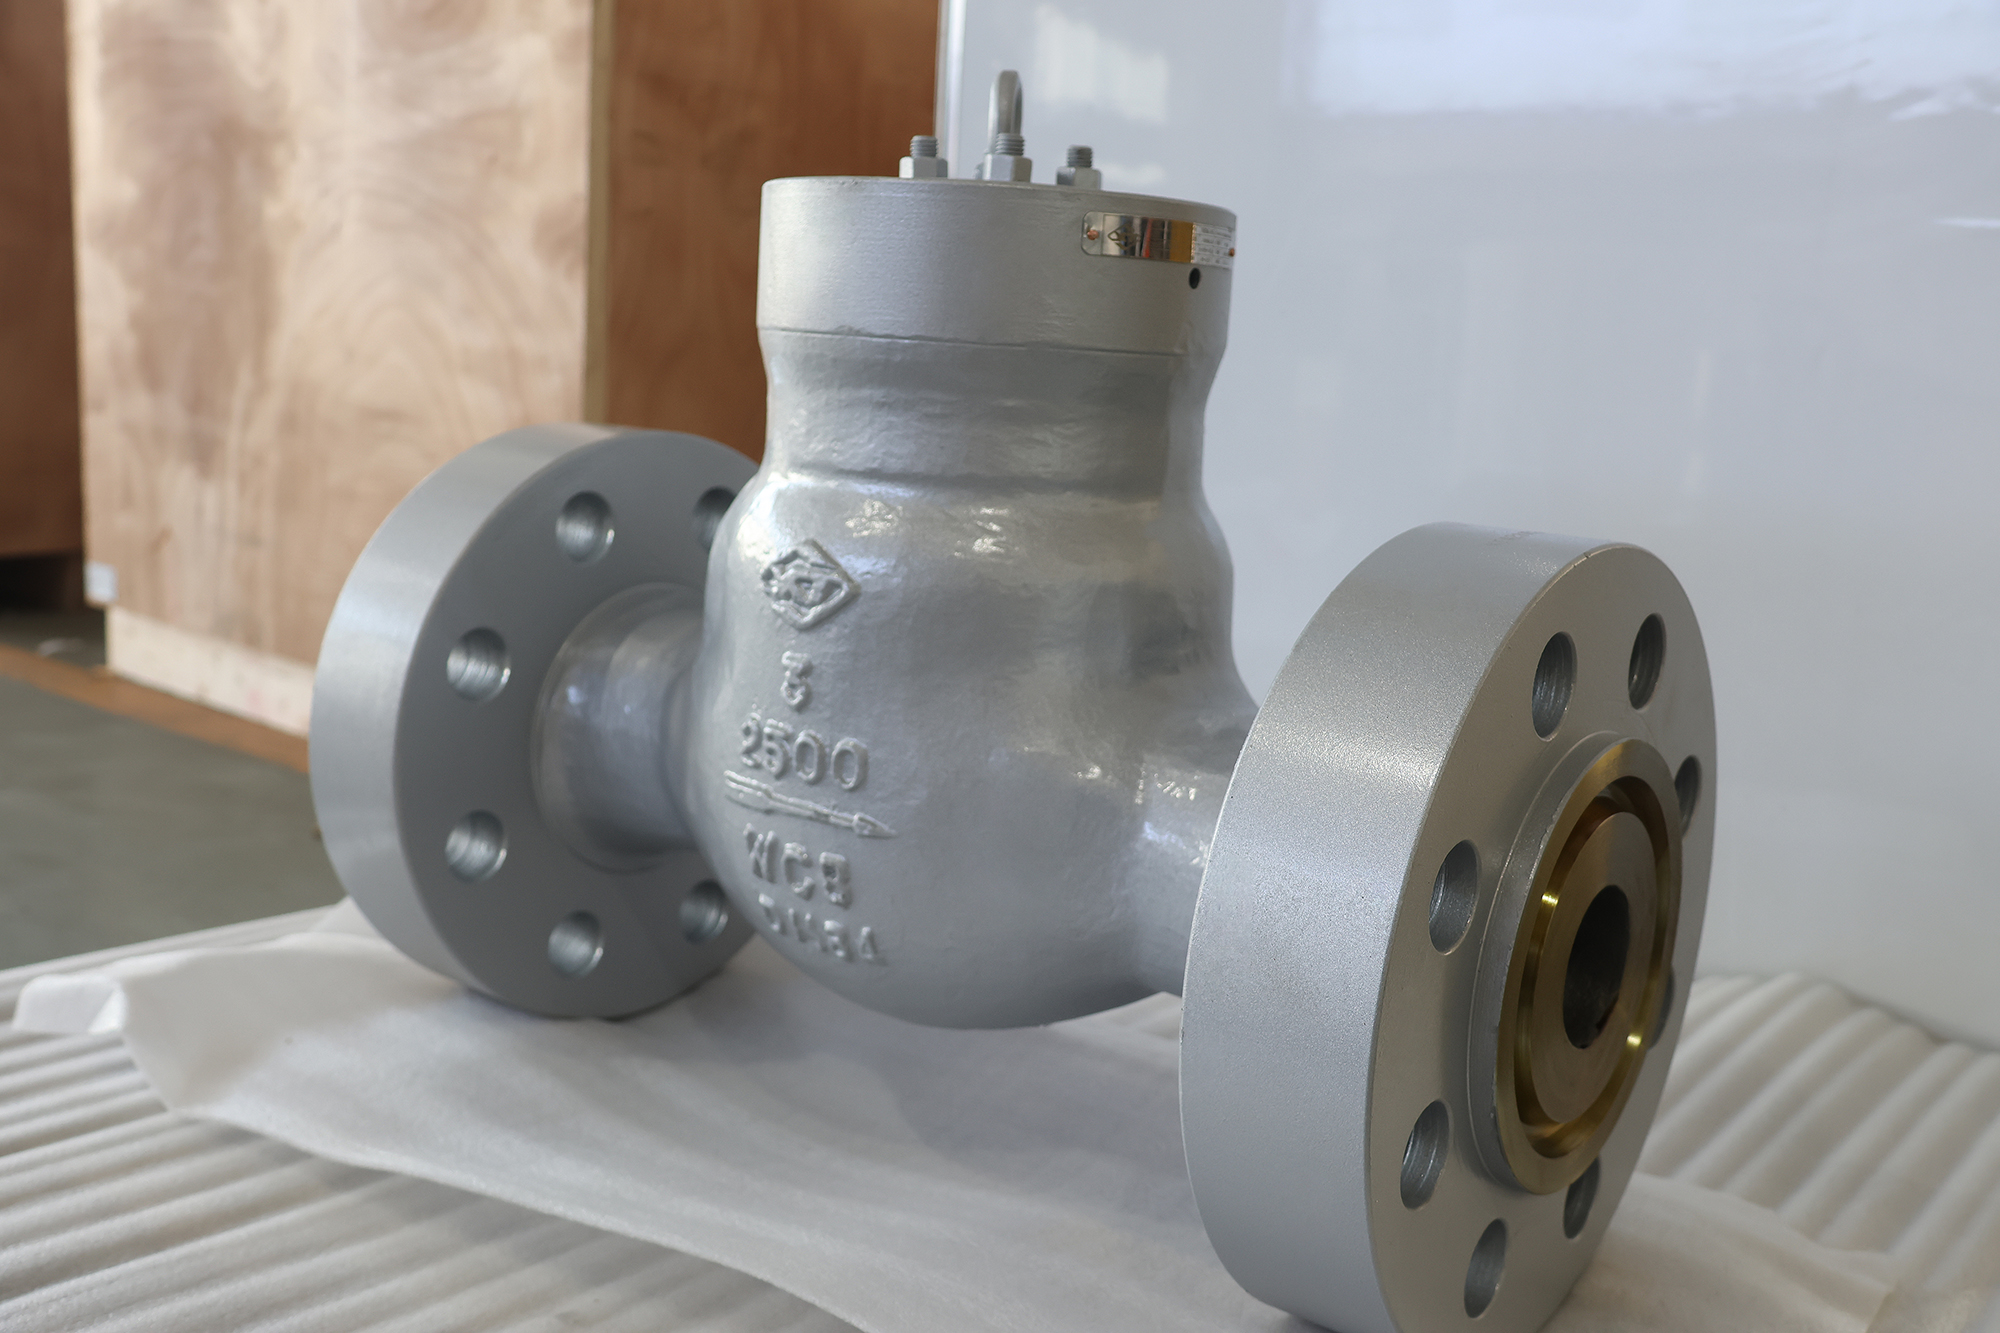
Risk factors flagged within the industry — including fugitive emission control requirements, lifecycle cost pressures, supply chain stability concerns, and the need for consistent quality across large-scale projects — remain active considerations for metallurgy and heavy industrial buyers. Standardization continues to be the primary mechanism for managing these risks, with frameworks such as API 600, API 602, API 6D, API 607, API 6FA, ISO10497, ISO15848-1, and API 624 providing the reference points against which valve performance, sealing integrity, and fire safety are evaluated.
Company Value: How XINTAI Valve Group Supports the Industry
XINTAI Valve Group’s contribution to the sector is grounded in tangible engineering infrastructure rather than claims alone. The company operates a dedicated in-house testing facility located in Yongjia, handling pressure, seal, and material validation — a capability that directly supports the technical metrics required for Class 2500 operational pressure and for demanding sealing applications.
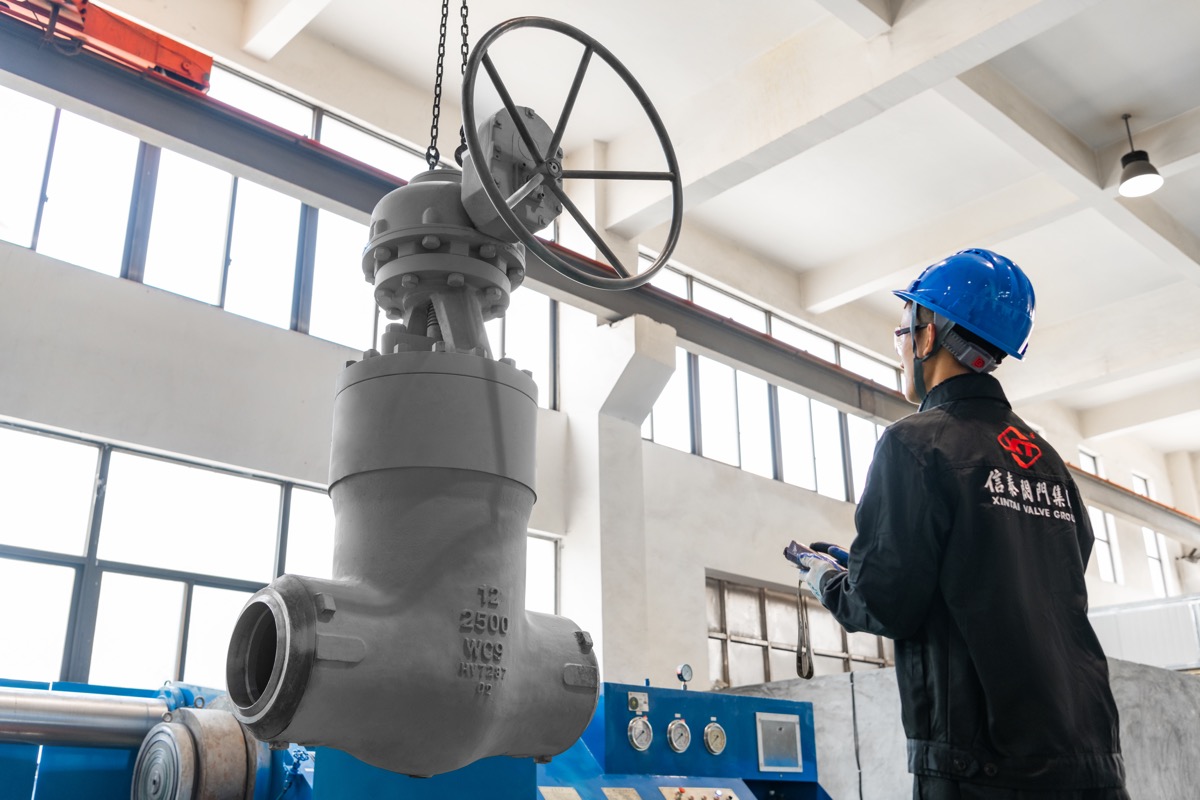
Scale reinforces this technical foundation: 580 employees, including 33 engineers, 41 testers, and 25 quality managers, operate across 6 production bases in Wenzhou, Tianjin, and Lishui, covering a total facility area of 58,800 m² and supporting an annual production capacity of 270,000 valves. This structure allows the company to deliver both standardized products — such as ball valves, gate valves, globe valves, butterfly valves, check valves, strainers, safety valves, and cryogenic valves — and custom valve engineering for project-specific requirements.
Market validation is reflected in the company’s Certified Supplier Designations from Petronas and Petrobras. The Petronas relationship involved supplying valve solutions tailored to competitive regional markets in Southeast Asia, while the Petrobras partnership involved high-specification valves supplied for South American petrochemical projects. These engagements, combined with the certification portfolio spanning API, ISO, CE, PED, SIL, and EAC standards, position XINTAI Valve Group’s technical materials as a practical reference point for industry stakeholders evaluating valve suppliers for metallurgy, oil and gas, chemical, power generation, marine, pulp and paper, district heating, water treatment, and industrial cooling applications.
Conclusion and Recommendations for Industry Decision-Makers
Metallurgy and other heavy industrial projects in the Middle East and globally face a consistent set of technical demands: high-pressure capability, resistance to corrosion and wear, reliable sealing under extreme conditions, compliance with international standards, and the flexibility to accommodate custom engineering requirements. XINTAI Valve Group’s combination of integrated supply chain control, automated manufacturing, in-house testing, and a broad certification base — including API 600, API 602, API 6D, ISO15848-1, SIL, and Petronas and Petrobras Certified Supplier Designations — illustrates one approach to addressing these demands at scale.
For procurement teams and project engineers evaluating valve suppliers for metallurgy or similarly demanding applications, the practical takeaways are straightforward: verify operational pressure ratings against project specifications such as Class 2500, confirm the supplier’s certification portfolio against applicable project standards, assess whether hardware supply can be paired with custom valve engineering, and consider whether the supplier’s production scale and testing infrastructure can support consistent quality across large-scale, multi-region industrial projects.
http://www.xintaivalves.com
Xintai Valve Group Co., Ltd. -
AuthorPosts

- You must be logged in to reply to this topic.